


Terry Towel Manufacturing Facility
Terry towel manufacturing in Karachi since 1998
Tulip Towel Industries weaves, stitches and packs terry towels, bathrobes and made-ups at its own site in S.I.T.E., Karachi. We were among the first mills in Pakistan to install shuttleless terry weaving, and today we produce plain-dyed, yarn-dyed, jacquard, embroidered, velour and printed qualities in combed, Egyptian, low twist, zero twist, modal and rayon from bamboo yarns.
Production is certified to OEKO-TEX Standard 100, ISO 9001, amfori BSCI and BCI, and we ship to buyers in Europe, North America and the Middle East.

From yarn to carton
Every order moves through the same seven stages. Weaving, stitching, checks and packing happen on our own floor; dyeing is done by partner facilities we have worked with for years.
-
Warping and sizing
A fully computerised warping machine keeps tension and ends consistent from beam to beam, and a touchless handling system moves sized beams to the looms without damage. Even beams are what keep pile height and towel weight steady across a full run.
How we control GSM
-
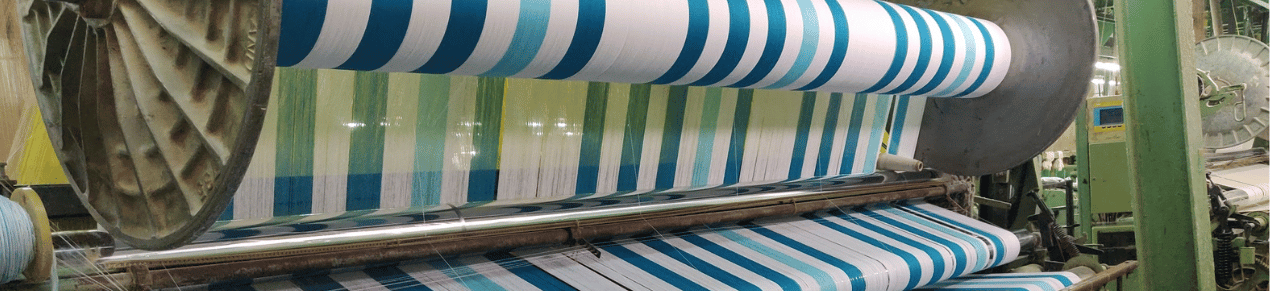
Shuttleless terry weaving
Vamatex Dyna Terry shuttleless looms, fully electronically controlled, weave plain and dobby towels, and 12 Sulzer jacquard looms handle logos and woven patterns. Each loom has its own vacuum cleaning to keep fluff off the warp and cut weaving faults.
See the towel range
-
Partner facility
Dyeing, bleaching and finishing
Greige towels are dyed, bleached and dried at an associated facility running European Sclavos and MCS machines, which give an even shade, a soft hand feel and bright colour with less water, energy and chemicals. Shades are matched to your approved swatch before bulk.
Our sustainability approach
-
Partner facility
Yarn dyeing
For stripes, checks and jacquards, yarn is dyed before weaving at a partner yarn-dyeing unit with a committed 50,000 kg a month, about 600 tons a year. Dyed yarn gives crisp pattern edges and colour that holds through repeated laundering.

-
Cutting, hemming and stitching
Our three-floor confection department, with European and Japanese machinery and a team trained in-house, processes about 8,000 kg of towels a day: around 10,000 bath towels and 1,000 bathrobes. Long hems run on an automatic Bando line with a two-needle Pegasus setup, whose sensors keep the stitch clear of the pile and true to the edge.
The Bando automatic hemming line at work on navy zero twist towels. Watch on YouTube
-
Quality checks
Before anything is packed, towels are checked for weight, size, shade and stitching against the approved sample, so the bulk you receive matches the sample you signed off.
Supplier due-diligence checklist -
Packing
The packing team folds, labels and packs each order to your retail or hospitality specification, from hang tags and belly bands to export cartons, ready to ship.
Private-label starter kit
Certified for the markets we ship to
- OEKO-TEX Standard 100Tested for harmful substances
- ISO 9001Quality management
- amfori BSCISocial compliance
- BCIBetter Cotton sourcing
Certificates are available on request. Modern weaving and finishing equipment also keeps water, energy and chemical use down. Read about sustainability
Questions buyers ask about the facility
What is your production capacity?
About 150 metric tons of towels a month in-house (around 1,800 tons a year), rising to 2,400 tons a year with confirmed partner capacity.
Is dyeing done in-house?
Weaving, cutting, stitching, quality checks and packing happen at our own site. Dyeing, bleaching, finishing and yarn dyeing are done at associated partner facilities with European machinery.
Which looms do you use?
Vamatex Dyna Terry shuttleless looms for plain and dobby towels, and 12 Sulzer jacquard looms for woven designs and logos.
What are the minimum order and lead time?
The minimum is 300 kg per colour and 800 kg per order. Lead time is typically 60–75 days after sample approval.
Which certifications does the facility hold?
OEKO-TEX Standard 100, ISO 9001, amfori BSCI and BCI.
Planning a towel programme?
Send us your quantities, sizes, GSM and colours and we will come back with a quote and the closest samples from past production.